


Remote Monitoring High Purity Nitrogen System
|
Model |
LPN - 100 |
LPN - 500 |
LPN - 1000 |
|
Purity Level |
99.999% |
99.999% |
99.999% |
|
Output Capacity (Nm³/h) |
100 |
500 |
1000 |
|
Power Supply |
220V/50Hz |
380V/50Hz |
380V/50Hz |
|
Remote Monitoring Features |
Real - time data display, Alerts for abnormal purity, Pressure & temperature tracking |
Advanced analytics, Predictive maintenance suggestions, Multi - device connectivity |
Customizable dashboards, Integration with plant-wide systems, 24/7 remote access |
|
Dimensions (L×W×H, mm) |
1200×800×1500 |
2000×1200×1800 |
2500×1500×2000 |
|
Certifications |
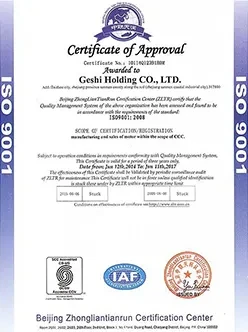
CE, ISO 9001 |
CE, ISO 9001, ISO 14001 |
CE, ISO 9001, ISO 14001, OHSAS 18001 |
Our factory & quipment
LDH GAS SYSTEMS COMPANY LIMITED


Advantages of the Remote Monitoring High Purity Nitrogen System
The Remote Monitoring High Purity Nitrogen System offers several distinct advantages that set it apart in the market.
Its remote monitoring capabilities revolutionize the way nitrogen systems are managed.
With real - time data access from any location via a secure network connection, operators can monitor key parameters such as nitrogen purity, pressure, temperature, and flow rate. This eliminates the need for constant on - site inspections, saving both time and labor costs. In case of any anomalies, immediate alerts are sent to designated personnel, enabling quick response times and minimizing downtime.

Technical Highlights of the System
At the heart of the Remote Monitoring High Purity Nitrogen System lies a combination of cutting - edge technologies. The remote monitoring functionality is powered by a sophisticated IoT (Internet of Things) platform. This platform integrates sensors placed strategically throughout the system to collect data on various parameters. The data is then transmitted via secure communication protocols, such as 4G/5G or Wi - Fi, to a cloud - based server. Here, advanced data analytics algorithms process the information, generating actionable insights and predictive maintenance schedules.
For purity control, the system employs a multi - stage purification process. It starts with pressure swing adsorption (PSA) or membrane separation technology to initially separate nitrogen from other gases in the air. Subsequently, additional purification stages, including catalytic oxidation and ultra - fine filtration, are used to remove trace amounts of residual impurities. Smart sensors continuously monitor the purity level, and if any deviation is detected, the system automatically initiates corrective actions, such as adjusting the flow rate or increasing the purification time.
The system's control unit is based on a high - performance programmable logic controller (PLC). This PLC coordinates the operation of all components, ensuring seamless integration and precise control. It also enables easy customization of the system's settings to meet specific customer requirements, whether it's adjusting the output capacity or modifying the remote monitoring parameters.

Certifications
Efficiently provide professional nitrogen solutions for all customers

Hot Tags: remote monitoring high purity nitrogen system, China remote monitoring high purity nitrogen system manufacturers, factory, High Purity N2 Generator, High Purity Nitrogen for Electronics Manufacturing, High Purity Nitrogen Generator for Laboratory Research, Low Maintenance High Purity Nitrogen Generator, nitrogen gas purity standards, Remote Monitoring High Purity Nitrogen System